English
 русский
 Français
 Español
 عربى
Paper Honeycomb Cleanroom Panel: Lightweight Wall and Ceiling Systems for Controlled Environments
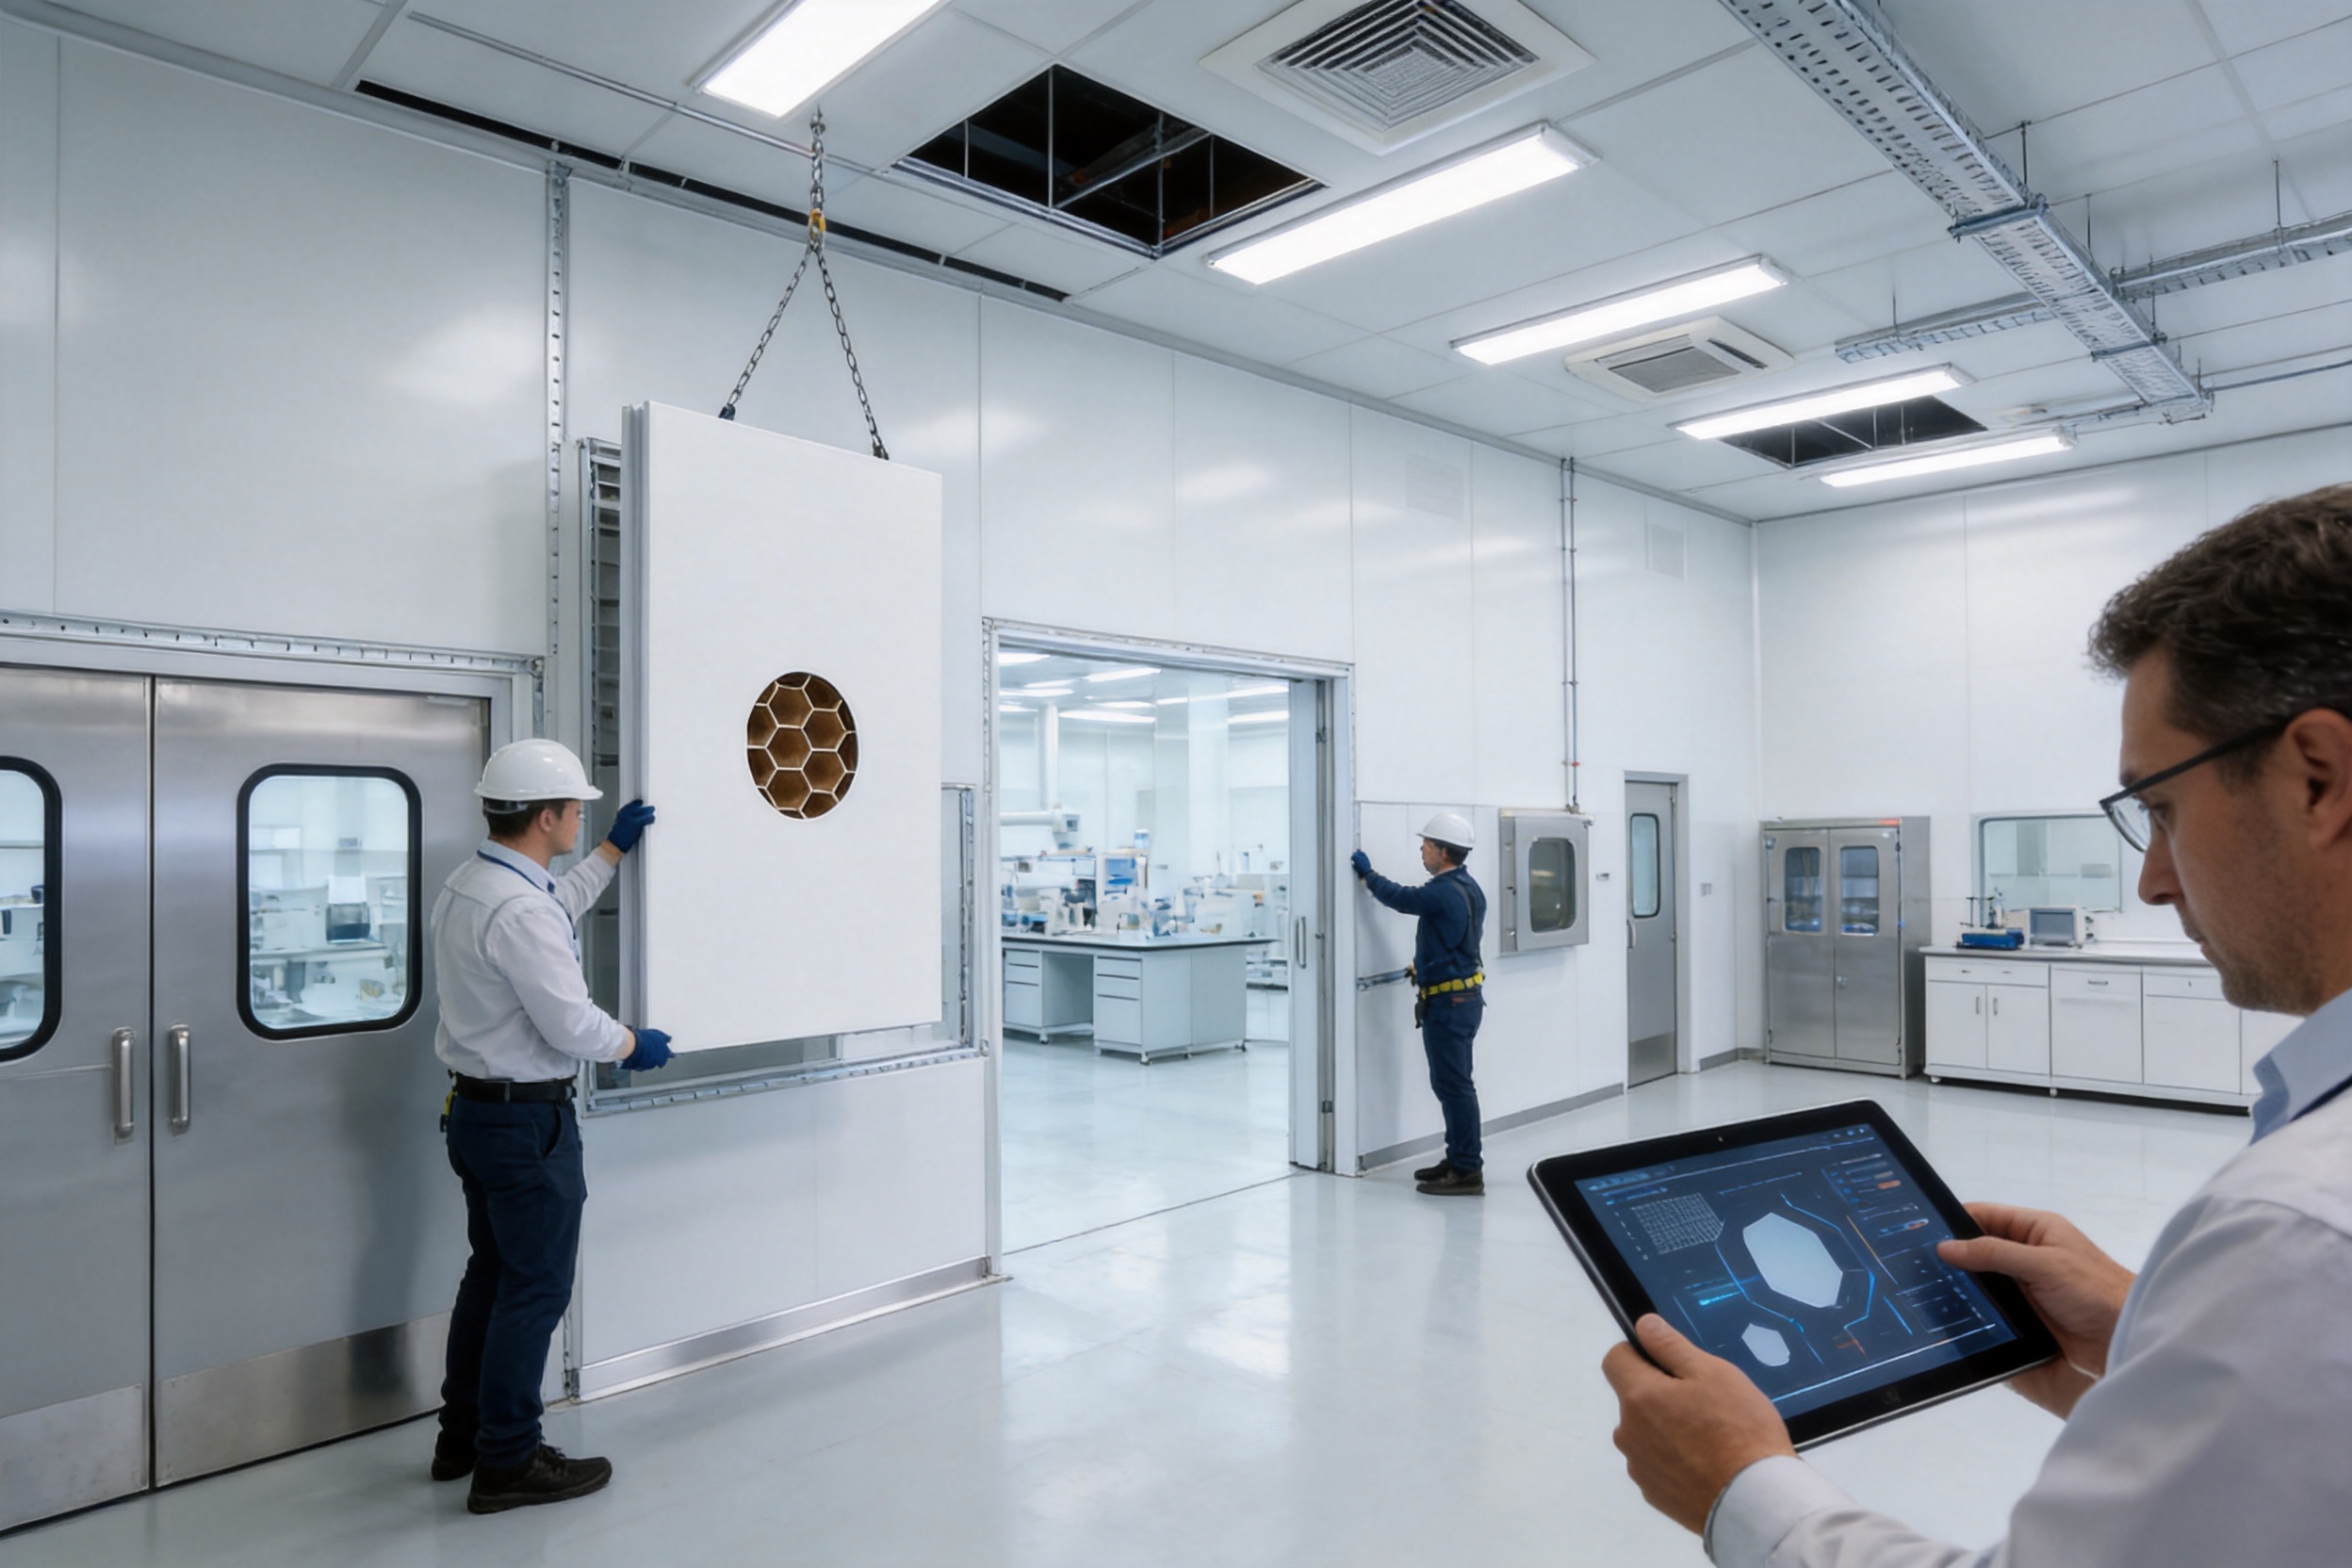
Paper Honeycomb Cleanroom Panel is a lightweight architectural panel developed for the construction of hygienic, controlled, and easily maintained interior environments. It is suitable for pharmaceutical factories, laboratories, hospitals, electronics workshops, food-processing areas, medical facilities, and other applications where cleanable surfaces, dimensional stability, efficient installation, and controlled operating conditions are important.
The panel combines a high-strength honeycomb structure with protective surface materials such as pre-coated steel, stainless steel, high-pressure laminate, or other project-specific finishes. This combination creates a wall and ceiling element that is easier to handle than many traditional solid-core alternatives while still providing the rigidity and flatness required for professional cleanroom construction.
For a cleanroom project, the panel is more than a simple partition board. It forms part of the room envelope, contributes to the separation of controlled areas, supports a smooth and hygienic interior finish, and influences the speed, quality, and cost of installation. The selection of the core, facing material, joint system, dimensions, edge treatment, and accessories must therefore be coordinated with the room classification, cleaning method, environmental conditions, and mechanical services.
Paper Honeycomb Cleanroom Panel is particularly valuable when a project requires reduced structural loading, efficient logistics, quick assembly, and a clean appearance. Its low weight helps simplify transportation and handling, while its engineered core provides support to the external skins and helps maintain panel geometry during installation and service.
Paper Honeycomb Cleanroom Panel
What Is a Paper Honeycomb Cleanroom Panel?
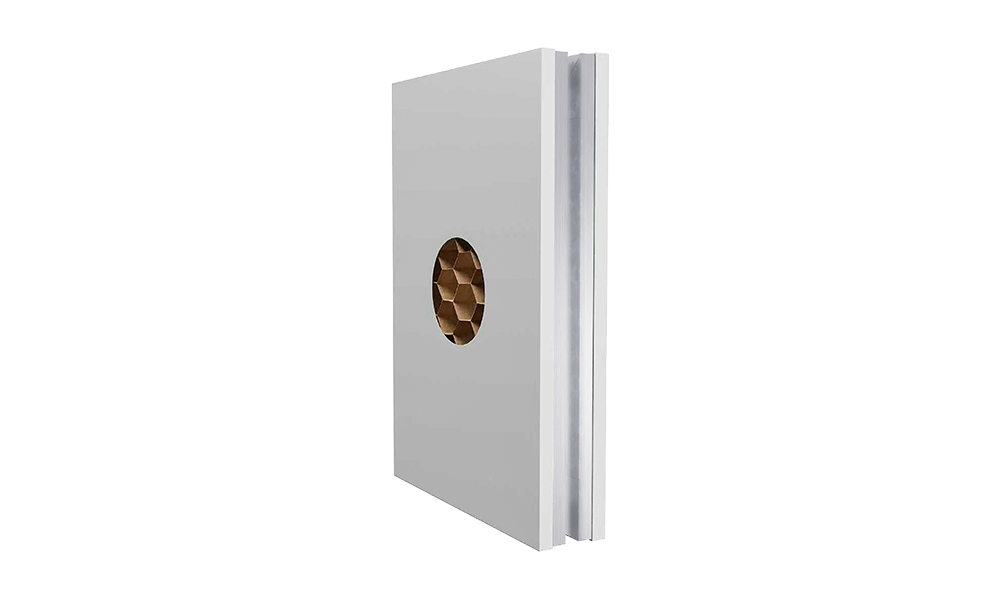
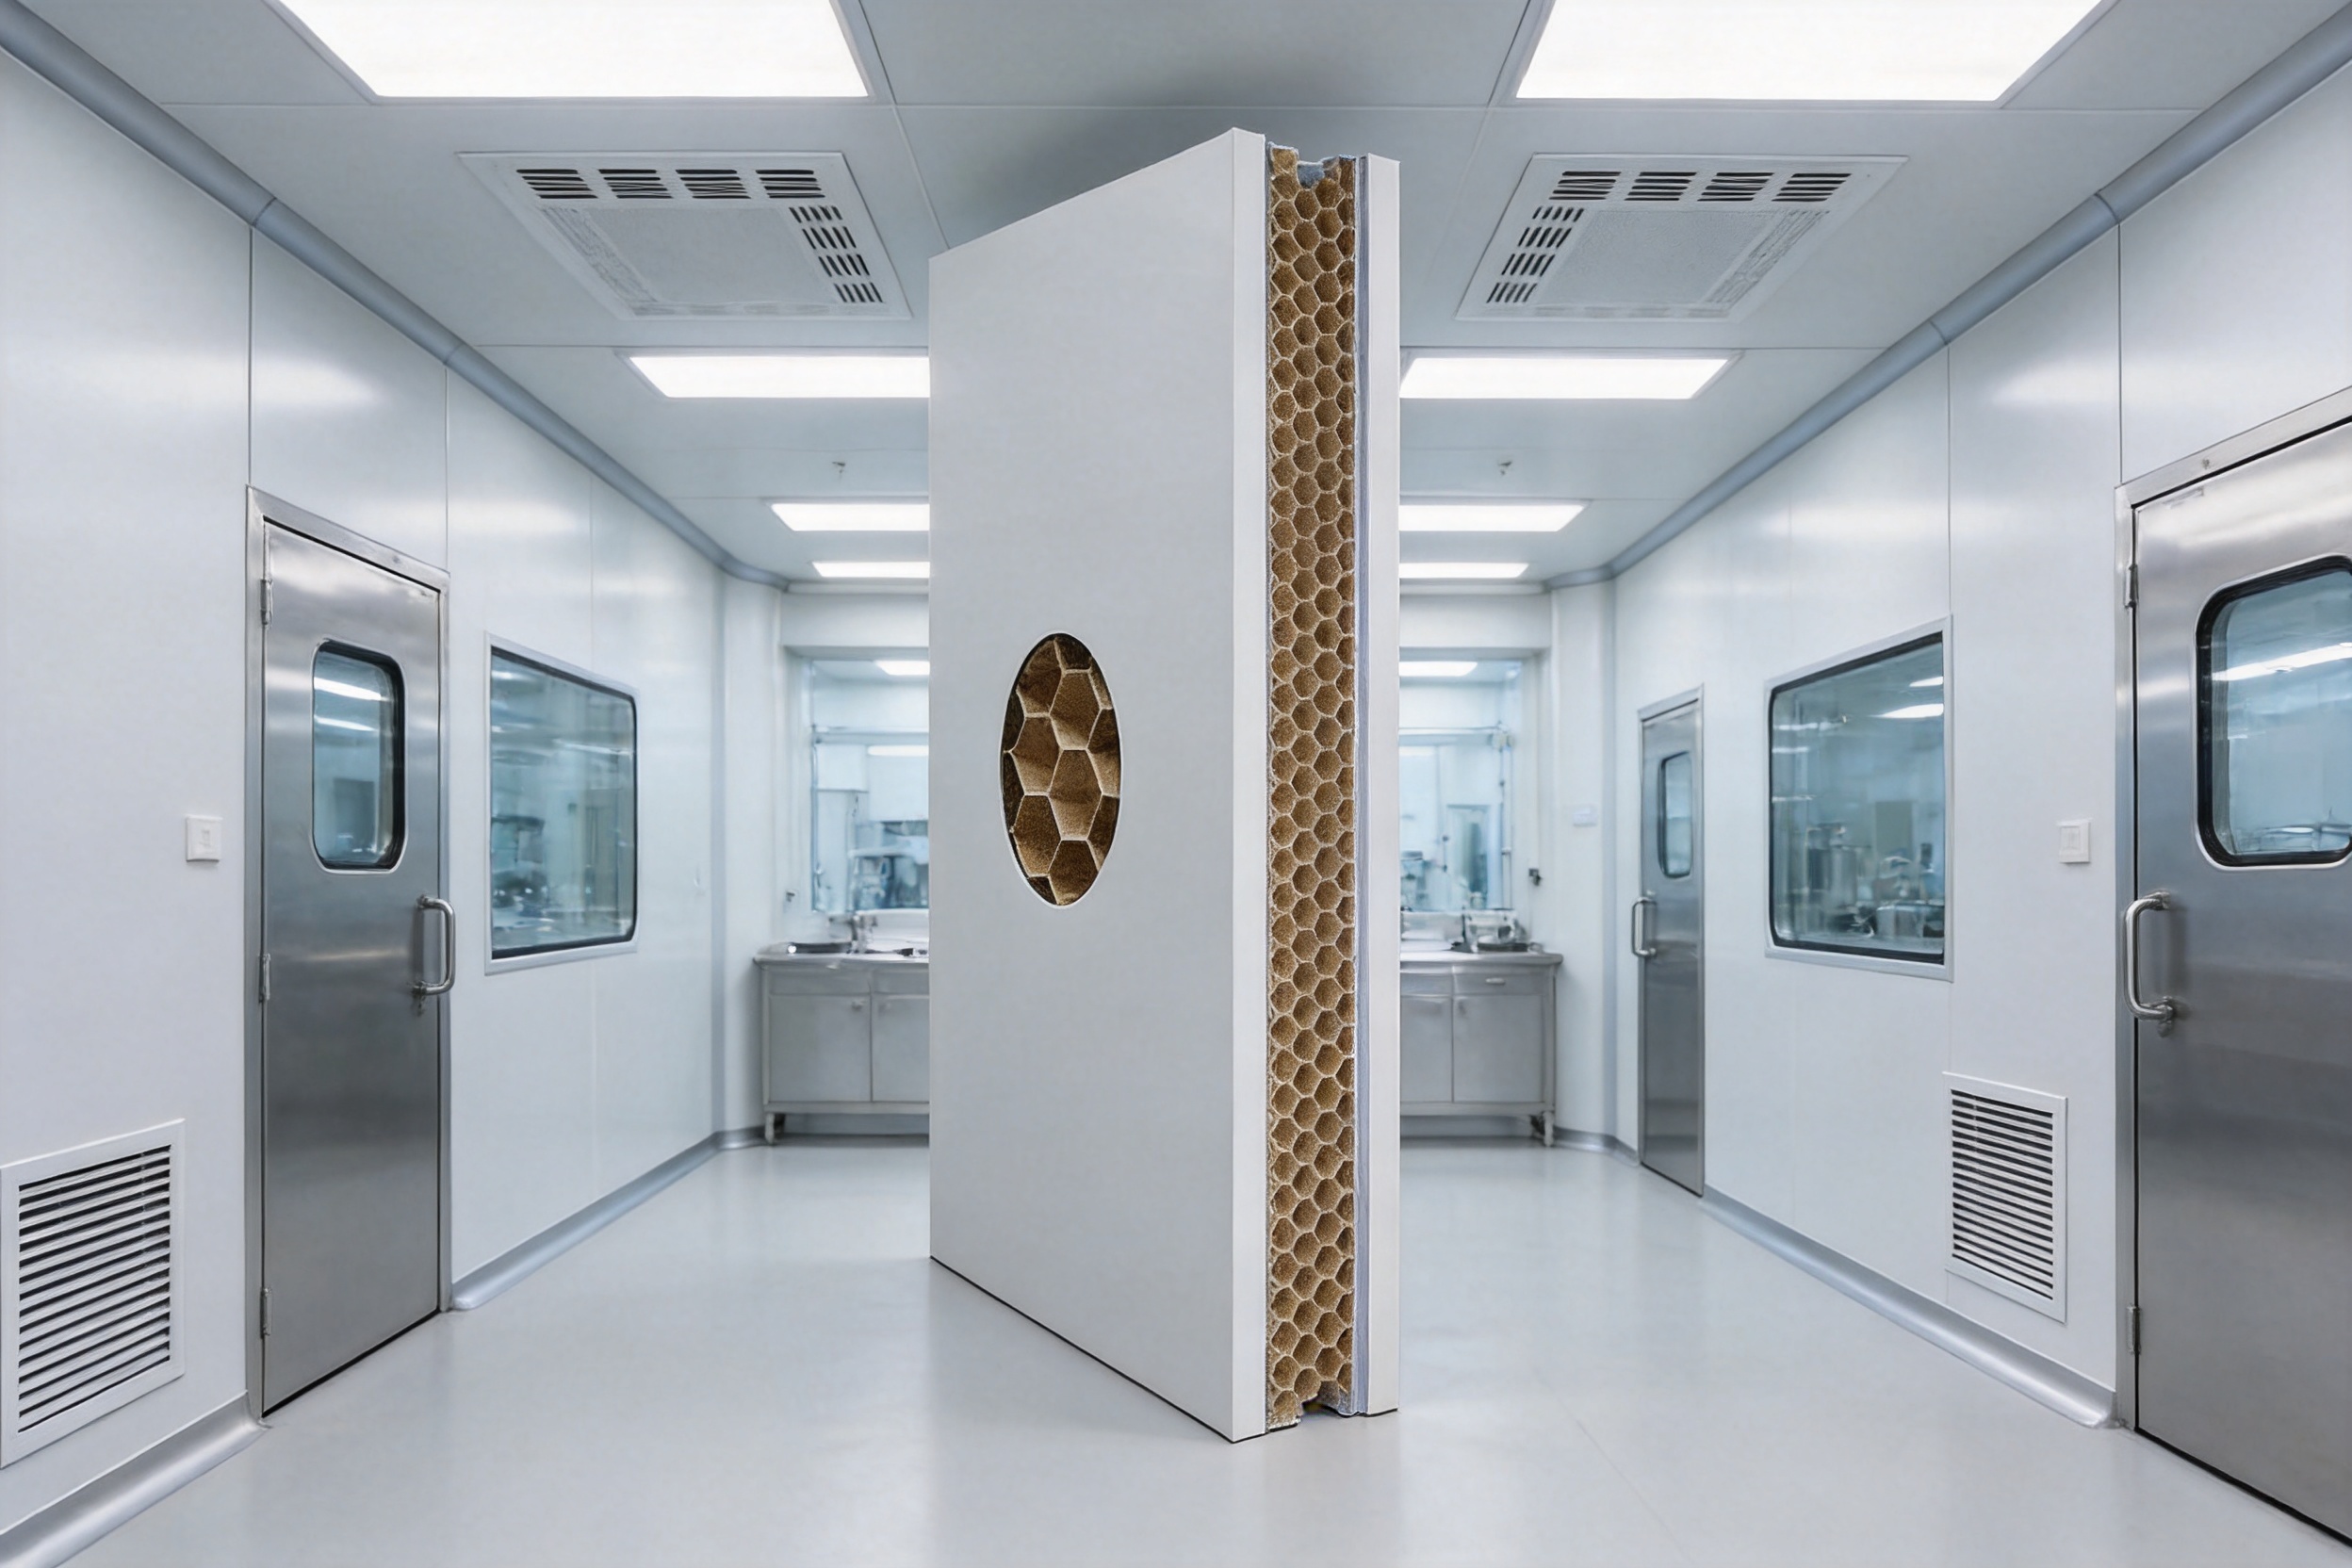
A Paper Honeycomb Cleanroom Panel is a prefabricated sandwich panel in which a cellular paper honeycomb core is bonded between two protective face sheets. The core consists of a regular network of cells that distributes loads across the panel and provides internal support to the external surfaces. The face sheets form the visible and cleanable sides of the wall or ceiling system.
The honeycomb structure uses material efficiently. Instead of filling the entire panel volume with a heavy solid material, it places structural material where it contributes most effectively to stiffness. This design principle allows the panel to achieve a useful balance between weight, rigidity, transportability, and surface flatness.
Depending on the project, the external surfaces may be manufactured from pre-painted galvanized steel, pre-painted steel, stainless steel, high-pressure laminate, or other approved materials. The selected facing affects chemical resistance, appearance, scratch resistance, cleaning compatibility, and long-term maintenance requirements.
Panel thicknesses commonly include 50 mm, 75 mm, and 100 mm. Other thicknesses, including 60 mm and 80 mm, may be available according to project requirements. The final panel construction should be selected after reviewing span, fixing method, ceiling configuration, service openings, environmental exposure, and the performance requirements of the facility.
In cleanroom construction, the panel is normally installed as part of a coordinated system. This system may include floor coving, ceiling suspension components, aluminum or steel profiles, doors, observation windows, pass boxes, air-return details, service penetrations, sealants, and other accessories. A properly engineered connection between these components is essential for achieving a durable and maintainable room envelope.
Core Structure and Material Configuration
The defining feature of this panel is its cellular paper honeycomb core. The core is arranged in repeated cells that support the face sheets and limit excessive movement across the panel surface. The exact density, cell geometry, adhesive system, and manufacturing method should be specified according to the intended application.
A honeycomb core can provide good rigidity without adding unnecessary mass. This is useful in projects where the existing building has load limitations, where panels must be carried through narrow access routes, or where installation takes place at height. Lightweight components can reduce the physical effort required from installation teams and can also lower the need for heavy lifting equipment.
The supplied information also identifies rockwool as an infill material in the product parameter table. Because a paper honeycomb core and a rockwool core are different constructions, the final technical specification should be confirmed before production. Some projects may require a paper honeycomb configuration, while other projects may use a mineral wool or rockwool configuration for different thermal, acoustic, or fire-related objectives. The core material must never be assumed solely from the product name.
Pharma United Co., Ltd. can coordinate the panel construction with the project specification so that the selected core, facing, thickness, and accessories match the intended use. This configuration-based approach is important because cleanroom projects often combine several performance objectives. A pharmaceutical manufacturing room, for example, may prioritize cleanability and chemical resistance, while an industrial electronics area may place greater emphasis on dimensional stability, low particulate generation, and efficient integration with ceiling-mounted services.
The face sheets are bonded to the core to create a composite panel. The quality of this bond affects surface flatness, resistance to separation, and long-term reliability. Manufacturing controls should therefore cover surface preparation, adhesive application, pressing or curing conditions, alignment, and inspection of the completed panel.
Available Surface Finishes
Surface selection is one of the most important decisions in cleanroom panel design. A cleanroom wall or ceiling surface must be compatible with the cleaning agents, disinfectants, temperature, humidity, and operating practices expected in the facility.
HPL, or high-pressure laminate, can provide a visually clean and durable surface for many controlled environments. It is available in different colors and patterns and can be selected where appearance, cleanability, and resistance to routine use are important.
HPGI refers to hot-dip galvanized steel with a protective coating or finish. It can offer a practical balance between corrosion protection, durability, appearance, and cost. PPGI, or pre-painted galvanized iron or steel, provides a factory-applied coated surface that can be selected in a range of colors and finishes.
SS304 stainless steel is often selected for areas requiring enhanced corrosion resistance and a robust hygienic surface. It may be suitable for rooms exposed to frequent cleaning, moisture, or more demanding sanitation procedures. The exact grade, surface finish, welding details, edge treatment, and cleaning chemicals should be reviewed for each application.
Asepticlean finishes are intended for applications where a highly hygienic and easy-to-clean surface is required. The final suitability of any finish depends on the complete system design, including joints, corners, penetrations, sealants, and cleaning procedures. A high-quality face sheet cannot compensate for poorly sealed joints or unsuitable accessories.
The standard surface thickness listed for the product is 0.6 mm or 0.8 mm. The correct thickness depends on the desired durability, panel dimensions, handling conditions, equipment contact, and project budget. Thicker skins can provide additional resistance to local impact and handling damage, but the complete panel must be engineered as a coordinated assembly.
Key Advantages Compared with Conventional Solid-Core Panels
Reduced Weight
The most immediate advantage of a paper honeycomb panel is its low weight. A cellular core uses less material than a fully solid core while still supporting the face sheets. This can reduce the weight of individual panels and make them easier to move from the delivery area to the installation location.
Reduced weight may also benefit the building structure. When many wall and ceiling panels are installed across a large facility, the cumulative dead load can be significant. A lightweight system can help reduce the load transferred to supporting structures, although structural calculations must always be completed by the responsible project engineer.
Efficient Transportation and Handling
Lightweight panels can improve logistics throughout the project. More panels may be handled with less effort, and installation teams can often position panels more efficiently. This is particularly useful in facilities with multiple rooms, limited access, long internal routes, or elevated ceiling systems.
Lower handling weight does not remove the need for proper protection. Panels should still be stacked on suitable supports, protected from moisture and impact, and moved according to the manufacturer’s instructions. Cleanroom products should be stored in a way that prevents contamination before installation.
Good Flatness and Rigidity
The repeated honeycomb geometry supports the face sheets and helps the completed panel maintain a smooth appearance. Good flatness is important in cleanrooms because uneven surfaces collect dust more easily, create visual defects, and complicate the sealing of joints and accessories.
Rigidity is also important when panels are used in long wall runs, ceiling grids, or areas containing service openings. The final performance depends on core density, panel thickness, face-sheet material, adhesive bonding, support spacing, and connection details. Proper engineering is therefore necessary rather than relying only on nominal thickness.
Fast Installation
Prefabricated cleanroom panels can shorten the time required for enclosure construction compared with conventional site-built wall systems. Panels are manufactured to defined dimensions, transported to the project, and installed using coordinated profiles and fixing components.
Faster installation can reduce the duration of general construction activities and allow other trades to begin their work sooner. It can also reduce the period during which a partially completed cleanroom is exposed to construction dust and accidental damage.
Easy Maintenance
A smooth panel surface is easier to wipe, disinfect, and inspect than an irregular or porous construction. When panel joints are correctly sealed and corners are detailed with suitable coving or trim, the room envelope becomes simpler to maintain.
Maintenance also benefits from modular construction. Individual panels, doors, windows, or accessories can potentially be repaired or replaced without demolishing the entire room. The actual replacement method depends on the installation system and should be considered during design.
Flexible Appearance and Specification
The availability of HPL, HPGI, PPGI, stainless steel, Asepticlean, and other surfaces allows the system to be adapted to different industries and budgets. Color selection can support room identification, zoning, and facility aesthetics, while stainless steel or specialized hygienic surfaces may be chosen for demanding areas.
Different thicknesses and core configurations also allow the panel to be matched to the application. This flexibility is a competitive advantage over systems that offer only one fixed construction.
Cleanroom Performance Considerations
A cleanroom panel does not create a compliant cleanroom by itself. Room performance is achieved by integrating the enclosure with filtration, air handling, pressure control, temperature control, humidity control, personnel procedures, material flow, and cleaning protocols.
The panel system nevertheless plays a central role. Walls and ceilings must help separate rooms, limit uncontrolled air movement, provide cleanable surfaces, and accommodate penetrations without creating difficult-to-maintain gaps. The panel joints must be accurately aligned and sealed with materials compatible with the operating environment.
For pharmaceutical and healthcare projects, the surface finish should be evaluated for resistance to the cleaning and disinfection chemicals used by the facility. For electronics applications, the design may need to address particulate control, electrostatic considerations, and the placement of technical services. For hospitals, the project may prioritize hygiene, durability, and integration with medical support areas.
The panel should be considered together with doors and windows. Poorly coordinated openings can compromise the appearance and performance of an otherwise well-built wall. Door frames, vision panels, transfer hatches, and utility penetrations should be detailed before panel production wherever possible.
Ceiling applications require particular attention to suspension, access, lighting, air terminals, filters, sprinklers, cable trays, and maintenance loads. A ceiling panel that is suitable for a wall is not automatically suitable for every ceiling arrangement. The support system and allowable loads must be confirmed for the actual design.
Manufacturing Process
Project Review and Technical Confirmation
Manufacturing begins with a review of the project requirements. This includes the room layout, panel dimensions, thickness, core material, surface finish, color, joint type, door and window positions, ceiling arrangement, and required accessories.
At this stage, any inconsistency between general product information and project-specific requirements should be resolved. For example, the stated product name identifies a paper honeycomb panel, while the parameter information lists rockwool as the infill material. A professional supplier should confirm whether the order requires paper honeycomb, rockwool, or another approved core before issuing production drawings.
Pharma United’s engineering team can support this coordination process with layout review, material selection, and BIM visualization where required. Early technical confirmation helps avoid cutting errors, mismatched components, and delays during installation.
Material Inspection
Incoming materials should be inspected before entering production. Core materials are checked for dimensions, density, moisture condition, and visible defects. Face sheets are reviewed for thickness, coating quality, color consistency, scratches, dents, and edge condition.
Adhesives, sealants, protective films, profiles, and accessories should also be controlled. Materials need to be stored in suitable conditions to prevent moisture absorption, contamination, or damage. This is particularly important for paper-based materials and coated surfaces.
Core Preparation
The honeycomb core is prepared to the required panel dimensions. Cutting accuracy is important because gaps, uneven edges, or incorrect core placement can affect bonding and panel geometry. The core should be handled carefully so that the cell structure is not crushed before lamination.
Where the design uses a different infill material, such as rockwool, the preparation process will follow the characteristics of that material. Density, cutting tolerance, edge support, and bonding requirements may differ. This is another reason why the core specification must be finalized before production.
Face-Sheet Preparation
Face sheets are cut according to approved production drawings. Surfaces may require cleaning, degreasing, abrasion, priming, or other preparation before adhesive application. The purpose is to create a reliable bond between the face sheet and core.
Protective films may be applied to reduce the risk of scratches during transportation and installation. Edges are checked for burrs and dimensional accuracy. If the project requires factory-made openings or special edge profiles, these operations should be completed using controlled equipment and verified against the drawings.
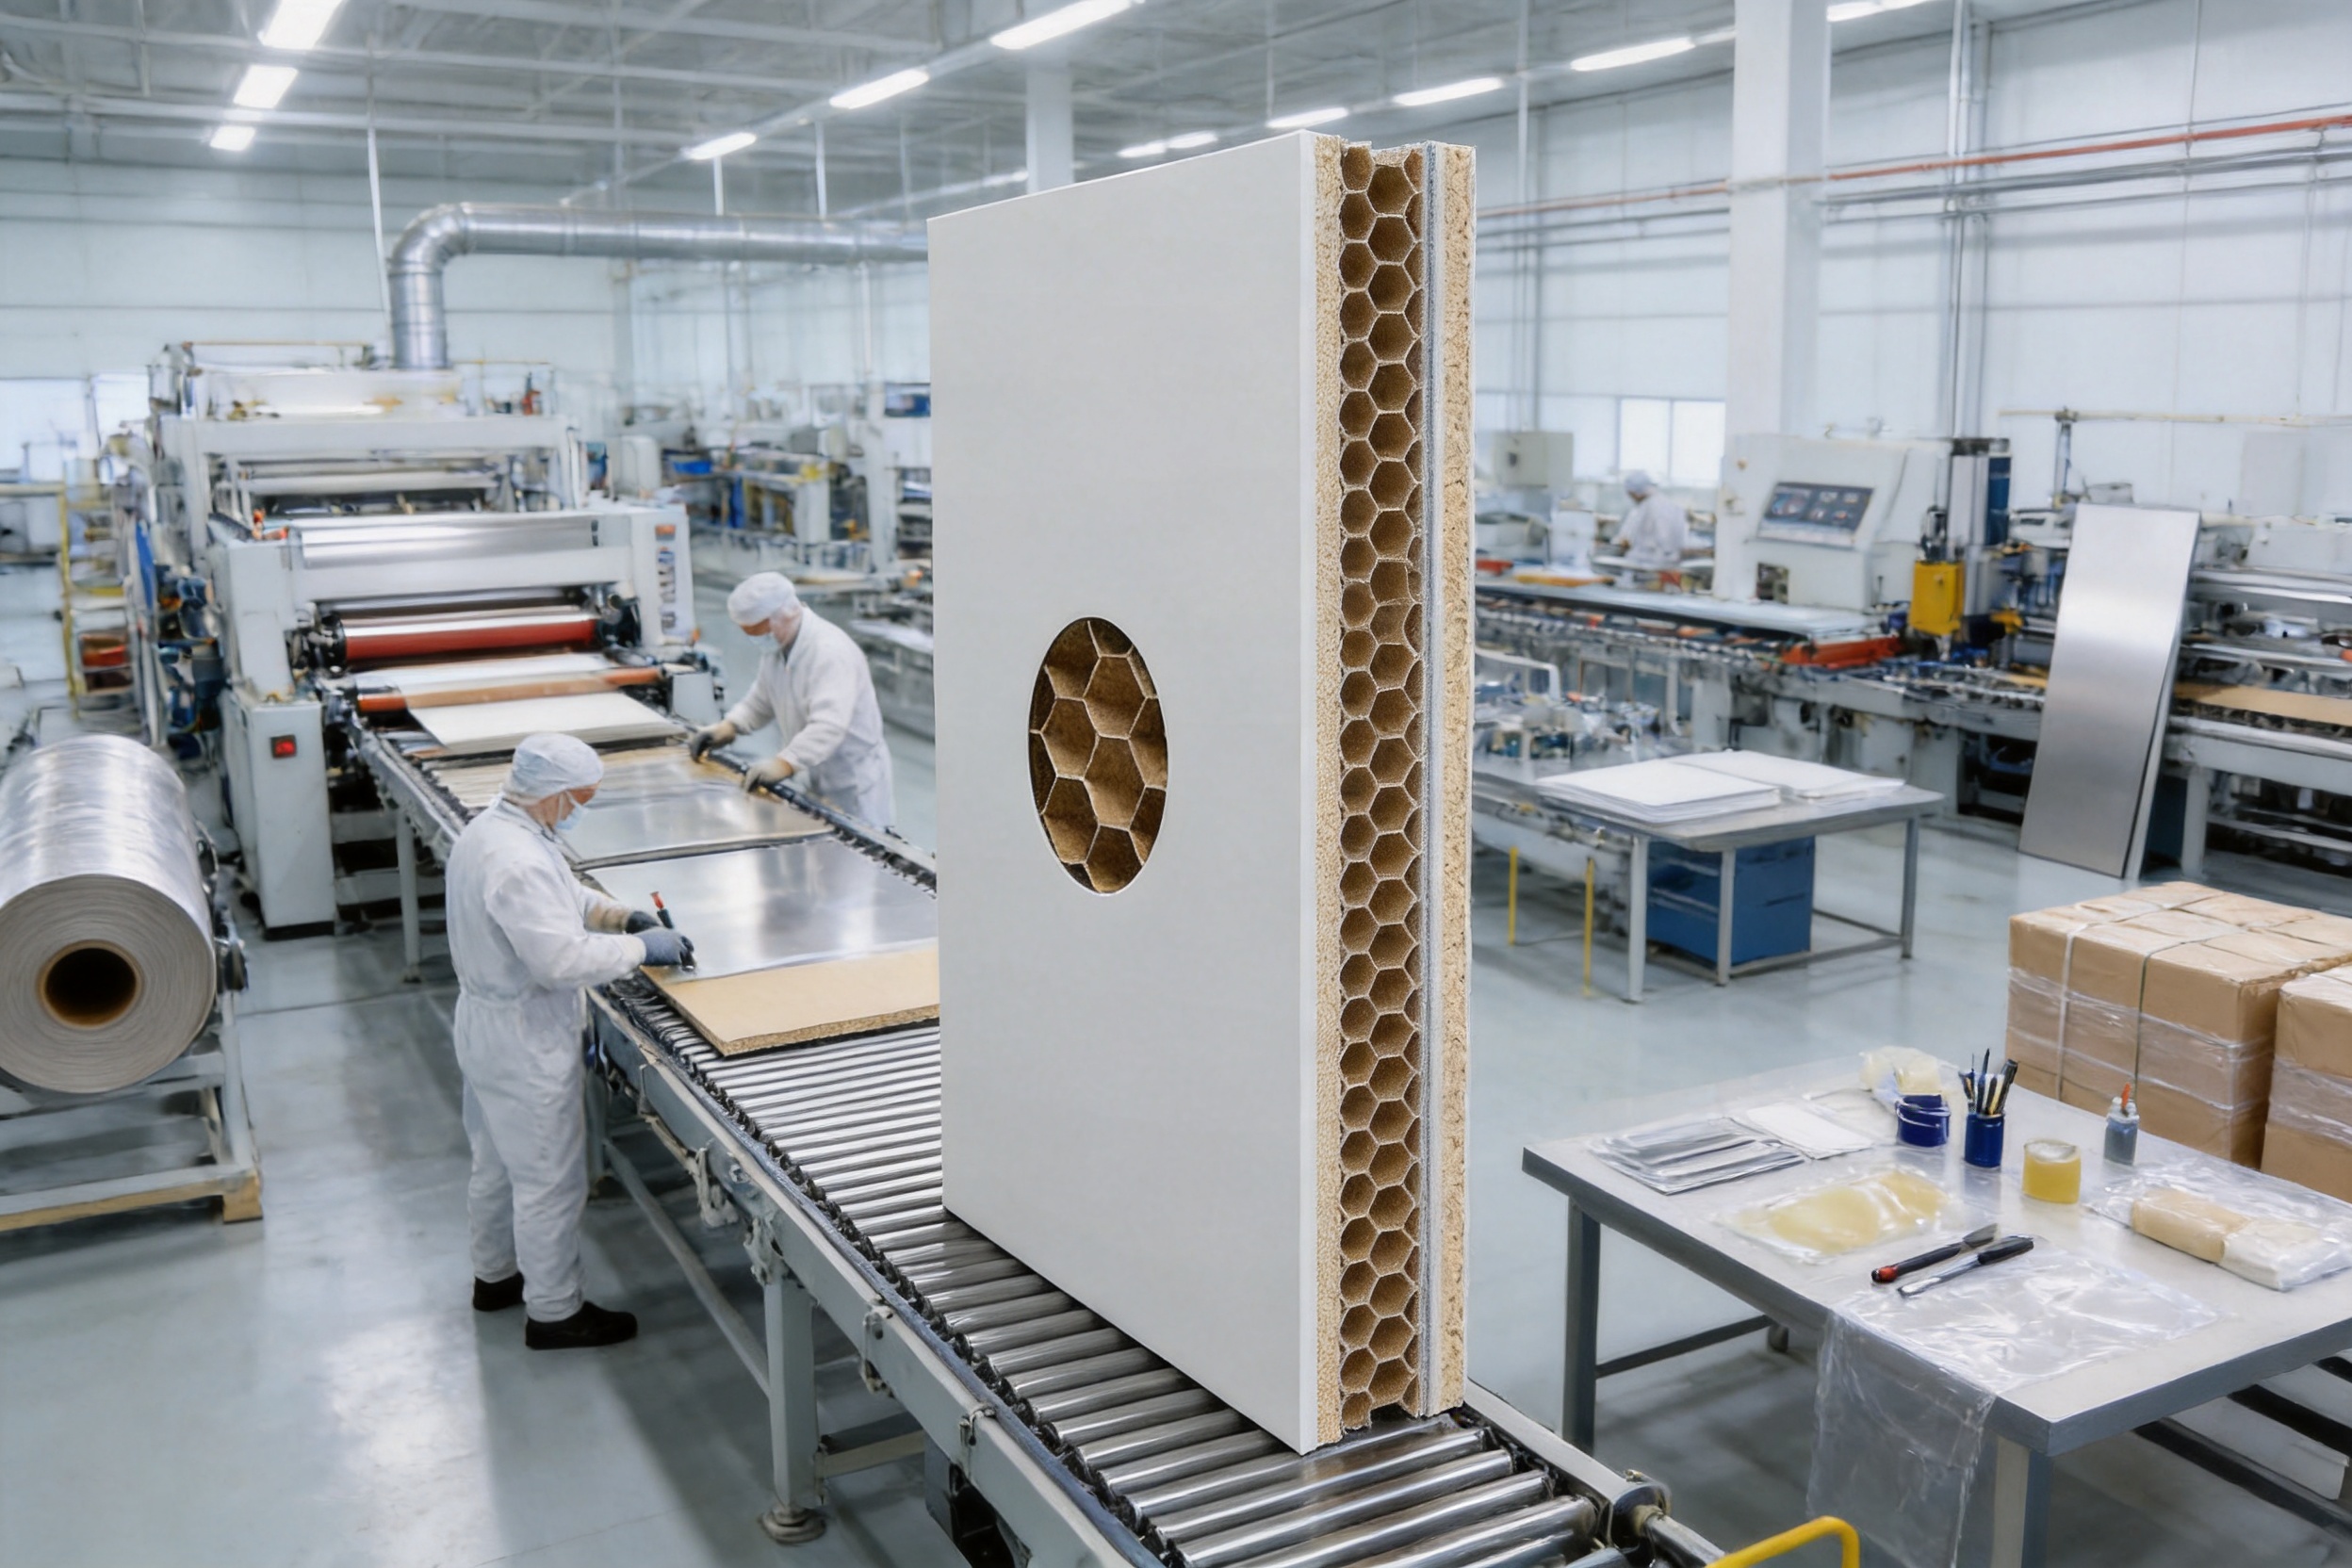
Adhesive Application and Lamination
Adhesive is applied according to the selected material combination and process parameters. Uniform application is essential. Too little adhesive can create weak areas, while excessive adhesive may affect panel thickness, curing, or surface flatness.
The core and face sheets are assembled in the correct sequence and aligned carefully. The assembly is then pressed or otherwise held under controlled conditions while the adhesive cures. Temperature, pressure, time, and positioning all influence the final quality of the panel.
Controlled lamination helps improve repeatability across production batches. It also reduces the risk of localized separation, face-sheet distortion, and inconsistent thickness. A modern manufacturing process should combine equipment-based control with operator inspection and documented procedures.
Panel Trimming and Edge Processing
After curing, panels are trimmed to their final dimensions. Edges may receive profiles, tongue-and-groove details, rebates, or other connection features depending on the system design. Accurate edge processing is important for achieving straight wall lines, reliable joints, and clean intersections.
Special panels may be manufactured for corners, door openings, window openings, service zones, ceiling transitions, or equipment interfaces. Factory preparation can reduce the amount of uncontrolled cutting required on site.
Inspection and Packing
Completed panels should be inspected for length, width, thickness, squareness, flatness, surface condition, edge quality, and visible bonding defects. The inspection procedure should identify panels that do not meet the approved requirements before they are packed.
Panels are then protected for transportation. Packaging should prevent rubbing between finished surfaces, protect corners, and limit exposure to moisture. Labels can identify panel numbers, dimensions, room locations, batch information, and installation orientation. Clear labeling is especially valuable for large projects containing many similar components.
Advanced Manufacturing Strengths
Pharma United Co., Ltd. operates its own manufacturing facility and provides cleanroom products alongside design, engineering, and installation services. This integrated structure can improve communication between the project team, production department, and installation personnel.
Having manufacturing capability in-house supports better control over material selection, production scheduling, quality coordination, and customization. It also allows technical feedback from completed projects to be incorporated into future designs.
The company reports more than 20 years of industry experience, an annual output of more than 1,000 40HQ containers, a factory area of approximately 20,000 square meters, and a workforce of more than 60 staff members. These resources indicate the ability to support both individual cleanroom packages and larger international projects.
The development history includes Shanghai Sinoarch Co., Ltd. in 2006, CESE International Co., Ltd. in 2014, the Kunshan factory and Pharma United Co., Ltd. in 2016, and a branch factory in Qianjiang, Hubei, in 2022. In 2026, the Kunshan factory expanded and doubled its previous production capacity. This development provides additional support for production planning, delivery coordination, and larger project workloads.
Production capacity alone is not enough to guarantee a successful cleanroom project. The more important advantage is the combination of manufacturing capability with engineering coordination. Panel dimensions must match the room layout, doors and windows must align with the wall system, and ceiling panels must coordinate with air-handling equipment and service openings.
Pharma United’s engineering team has more than 10 years of average on-site experience. This practical background can help identify installation risks before production and can support site teams during assembly. BIM visualization can also help clients review room layouts, equipment interfaces, and service coordination before materials are manufactured.
Integrated Cleanroom Engineering Capability
The Paper Honeycomb Cleanroom Panel is one element of a broader cleanroom solution. Pharma United’s product range includes metallic sandwich panels, HPL panels, cleanroom doors and windows, HVAC systems, and various cleanroom equipment.
This wider product range allows the supplier to coordinate related components instead of treating the wall panel as an isolated item. A complete package may include wall and ceiling panels, air-conditioning equipment, filtration systems, lighting, pass boxes, doors, windows, floor finishes, and installation services.
Integrated coordination can reduce interface problems between suppliers. For example, the position of a return-air opening may affect a wall panel joint, while a door frame may determine the required panel cutout. When these matters are reviewed by one engineering team, the project can benefit from clearer responsibility and fewer last-minute modifications.
The company provides turnkey services that include cleanroom design, material manufacturing, and on-site installation. This approach is suitable for clients that need support from the early planning stage through commissioning and handover.
International project experience across Africa, the Middle East, South Asia, and other markets also provides exposure to different construction environments, transportation conditions, labor practices, and approval procedures. Each project still requires local code review and client-specific technical approval, but international experience can strengthen practical project management.
Applications
Pharmaceutical Manufacturing
Pharmaceutical facilities require carefully controlled environments and surfaces that can be cleaned and maintained according to established procedures. Paper Honeycomb Cleanroom Panel can be used for internal walls and ceilings when the selected surface, joint treatment, core, and accessories meet the project requirements.
Typical areas may include material preparation rooms, weighing rooms, formulation spaces, packaging areas, sampling rooms, laboratories, airlocks, change rooms, and support corridors. The final design must be coordinated with pressure cascades, personnel movement, material flow, and equipment access.
Laboratories
Laboratories often require flexible partitions, cleanable surfaces, and convenient integration with utilities. The lightweight nature of the panel can be useful when layouts may be modified or when panels must be installed around existing building structures.
The surface finish should be selected according to the chemicals, solvents, disinfectants, and operating temperatures used in the laboratory. Worktop, sink, fume cupboard, and equipment interfaces should be reviewed separately.
Hospitals and Healthcare Facilities
Healthcare applications may include sterile areas, procedure rooms, diagnostic spaces, pharmaceutical preparation rooms, isolation areas, and technical support rooms. Panel systems can provide smooth walls and ceilings that support cleaning and visual inspection.
Healthcare projects often require careful coordination of medical gases, electrical services, lighting, ventilation, doors, observation windows, and impact-prone areas. The panel thickness and face-sheet material should be selected according to expected use.
Electronics Workshops
Electronics manufacturing and assembly areas may require low-particle interiors, stable surfaces, and efficient integration with technical services. A smooth panel system can support routine cleaning and help reduce locations where dust may accumulate.
Where electrostatic control is required, the complete room design should address flooring, grounding, personnel procedures, equipment, and panel surface characteristics. The wall panel should be evaluated as part of the total electrostatic-control strategy.
Food and Other Controlled Environments
Food-processing support areas, cosmetics production rooms, medical device facilities, and other controlled environments may also use cleanroom panel systems. The correct surface finish, core, joint design, and cleaning compatibility must be selected for each application.
Installation Recommendations
Before installation, the building structure should be checked for level, plumb, moisture, and readiness. Floors, ceilings, and supporting surfaces must be prepared so that the panel system can be installed accurately.
Panel locations should be marked according to approved drawings. Installation teams should verify panel numbers and orientation before fixing. Protective films should remain in place where possible until adjacent construction activities are complete.
Joints should be aligned consistently and sealed with the specified material. Sealant application should be continuous and free from gaps, voids, contamination, or excessive irregularity. Corners and wall-to-ceiling transitions require special attention because they are common locations for dust collection and cleaning difficulty.
Openings for electrical boxes, pipes, ducts, air terminals, lights, and other services should be made carefully. Uncontrolled cutting can damage the core, weaken the panel, or create an irregular opening. Factory-made openings are preferable when dimensions are known in advance.
During installation, panels should be protected from impacts, water, welding sparks, grinding dust, and other construction hazards. Cleanroom panels should not be used as temporary work platforms or supports for heavy materials.
After installation, the room should be cleaned progressively. Protective films, labels, adhesive residue, metal particles, and construction dust must be removed using methods compatible with the selected surface finish. Final cleaning and inspection should be completed before commissioning.
Quality Control and Project Documentation
Quality control should cover the entire process from design confirmation to final installation. Important documents may include approved shop drawings, material submittals, panel schedules, surface samples, inspection records, packing lists, installation instructions, and maintenance recommendations.
For larger projects, a panel schedule can identify each panel by location, dimension, finish, and orientation. This reduces confusion during delivery and installation. It also creates a useful record for future maintenance or replacement.
Sample panels or mock-ups can help clients confirm color, texture, joint appearance, corner treatment, and cleaning suitability before mass production. A mock-up is particularly valuable when several materials and accessories meet in one room.
Factory inspection can be arranged according to the project contract. Clients may review material condition, production methods, panel dimensions, surface finish, packaging, and documentation before shipment. The exact inspection scope should be agreed during procurement.
Performance claims should always be supported by the relevant technical documents. Fire behavior, thermal performance, acoustic performance, chemical resistance, load capacity, and hygiene suitability depend on the complete panel construction and should not be generalized from one configuration to another.
How to Select the Correct Configuration
The first step is to define the room function. A pharmaceutical filling area, a laboratory, an electronics workshop, and a hospital procedure room may all use cleanroom panels, but their cleaning routines and technical demands can differ substantially.
The second step is to select the core. Paper honeycomb may be preferred for lightweight construction and efficient handling. Rockwool or another core may be required where different thermal, acoustic, or fire-related properties are needed. The chosen core must be clearly identified in the technical submittal.
The third step is to select the face material. Stainless steel may be appropriate for demanding hygienic or corrosive environments, while coated steel or HPL may provide a practical solution for general cleanroom areas. Surface thickness should be selected according to durability and impact expectations.
The fourth step is to confirm panel thickness. Standard options include 50 mm, 75 mm, and 100 mm, with 60 mm and 80 mm also available in some configurations. Thickness selection should consider wall height, support spacing, ceiling span, services, access requirements, and structural conditions.
The fifth step is to coordinate openings and accessories. Doors, windows, pass boxes, return-air grilles, lights, filters, sprinklers, cable trays, and other systems should be shown on the approved layout before production.
The final step is to define installation and maintenance requirements. The client should understand how the panels will be transported, stored, installed, cleaned, repaired, and replaced. A well-defined maintenance plan can extend the useful life of the cleanroom envelope.
Comparison with Other Cleanroom Wall Systems
| Evaluation factor | Paper honeycomb panel | Traditional solid-core panel | Site-built wall construction |
|---|---|---|---|
| Weight | Generally lightweight because of the cellular core | Often heavier, depending on the core material | Varies according to framing, boards, insulation, and finishes |
| Handling | Convenient for transport and manual positioning when correctly sized | May require more labor or lifting support | Individual materials may be easy to handle, but assembly is more extensive |
| Surface flatness | Factory-laminated face sheets can provide a consistent smooth surface | Can provide good flatness when accurately manufactured | Depends heavily on site workmanship and finishing quality |
| Installation speed | Rapid prefabricated assembly with coordinated profiles | Rapid if supplied as a complete prefabricated system | Usually slower because several trades and wet processes may be involved |
| Customization | Available in different finishes, thicknesses, and configurations | May offer multiple core and face options | Highly flexible but may require more design and site coordination |
| Structural loading | Can help reduce dead load when the complete design is suitable | May impose a higher dead load | Depends on the complete wall build-up |
| Maintenance | Individual panels and accessories can be managed within a modular system | Also suitable for modular maintenance if correctly designed | Repairs may involve more disruption to finishes and services |
This comparison is general and does not replace project-specific engineering. The best system depends on the required core performance, room classification, local regulations, cleaning chemicals, fire strategy, budget, and construction schedule.
Environmental and Lifecycle Considerations
The lightweight design of a paper honeycomb panel can reduce transportation effort and structural loading. Lower weight may also reduce the quantity of supporting materials required in some applications, although the complete building design must be evaluated before making environmental conclusions.
Paper-based core materials may support efficient material use because the cellular structure provides stiffness with relatively low mass. Responsible sourcing, moisture protection, adhesive selection, production waste management, and end-of-life handling should be considered as part of the project’s sustainability strategy.
Long service life is another important lifecycle factor. A durable surface that can be cleaned and repaired may reduce the frequency of replacement. Proper installation is essential because damaged edges, leaking joints, and unsuitable cleaning agents can shorten the life of any panel system.
Clients should request the appropriate environmental and material information for the exact configuration being purchased. A paper honeycomb panel with a stainless-steel facing has different material characteristics from a panel with a coated steel or laminate facing.
Why Choose an Integrated Supplier?
An integrated supplier can provide more than a product catalogue. It can support the relationship between design, manufacturing, logistics, installation, and after-sales service. This is particularly useful when the project includes several cleanroom areas or when the client requires a turnkey solution.
Pharma United Co., Ltd. combines cleanroom engineering with manufacturing and installation capabilities. The company’s stated experience includes projects for pharmaceutical companies such as Sanofi and Novartis, as well as industrial plants in Africa, the Middle East, South Asia, and other international markets.
Its manufacturing base, engineering personnel, BIM capability, and international project experience can support different procurement models. A client may purchase panels only, request a coordinated material package, or engage the company for design, manufacturing, delivery, and on-site installation.
The company’s product range also allows the Paper Honeycomb Cleanroom Panel to be coordinated with cleanroom doors, windows, HVAC equipment, and other equipment. This reduces the risk of treating each component as an independent package.
Questions and Answers
What is the main advantage of a Paper Honeycomb Cleanroom Panel?
Its main advantage is the combination of low weight, useful rigidity, good surface flatness, and efficient installation. The cellular core can reduce the mass of the panel compared with many solid-core alternatives while supporting the external face sheets.
Can the panel be used for both walls and ceilings?
Yes, the panel is designed for wall and ceiling applications. However, ceiling use requires a review of suspension spacing, panel span, access requirements, service openings, and any additional loads. The wall specification should not automatically be applied to a ceiling without engineering confirmation.
Which surface finishes are available?
Available finishes include HPL, HPGI, PPGI, SS304, and Asepticlean. Other surface materials may be available according to the project requirements. The selected finish should be evaluated against cleaning chemicals, humidity, temperature, impact, and appearance expectations.
What panel thicknesses are available?
Common thicknesses are 50 mm, 75 mm, and 100 mm. Thicknesses of 60 mm and 80 mm may also be available. The final choice depends on the room design, support conditions, panel dimensions, and performance requirements.
Is the core always made from paper honeycomb?
The product name identifies a paper honeycomb construction, but the supplied parameter information also lists rockwool as an infill material. The exact core must therefore be confirmed in the technical specification and approved drawings before production.
Can the panel be customized?
Yes. Customization may include panel dimensions, thickness, surface material, color, edge details, openings, joint arrangements, and integration with doors, windows, air terminals, and other cleanroom accessories. Customization should be finalized during the engineering and shop-drawing stage.
Is the panel suitable for pharmaceutical facilities?
It can be suitable for pharmaceutical facilities when the selected configuration meets the project’s requirements for cleanability, surface durability, joint sealing, room classification, fire strategy, and other applicable criteria. The complete cleanroom system must be designed and validated as a whole.
Can the panel reduce construction time?
Prefabricated panels can reduce installation time because many components are manufactured to defined dimensions and assembled using coordinated profiles. Actual schedule savings depend on site readiness, drawing approval, logistics, labor, and the complexity of the room layout.
How should the panels be cleaned?
Cleaning procedures should follow the approved maintenance instructions for the selected face material. Operators should use compatible cleaning agents, suitable tools, and methods that do not scratch or damage the surface. Abrasive materials and unapproved chemicals should be avoided.
Does a lightweight panel require special handling?
It requires careful handling even though it is easier to move than a heavier panel. Panels should be protected from bending, crushing, moisture, edge damage, and surface scratches. Proper stacking and lifting procedures should be followed during delivery and installation.
Can the supplier provide installation services?
Pharma United Co., Ltd. provides on-site installation support as part of its cleanroom engineering services. The exact scope should be defined in the project contract, including supervision, labor, equipment, testing, cleaning, and handover documentation.
What information should be supplied for a quotation?
Useful information includes floor plans, room heights, wall and ceiling areas, required room classifications, panel thickness, core material, surface finish, color, door and window schedules, service openings, delivery location, installation requirements, and applicable standards.
Conclusion
Paper Honeycomb Cleanroom Panel provides a practical solution for cleanroom walls and ceilings where low weight, rigidity, flatness, efficient installation, and cleanable surfaces are required. Its cellular core can reduce handling effort and structural loading while supporting a prefabricated construction method suitable for pharmaceutical, laboratory, healthcare, electronics, and other controlled environments.
The strongest results are achieved when the panel is treated as part of an integrated cleanroom system. Core selection, face material, thickness, joints, accessories, doors, windows, ceiling supports, HVAC interfaces, and installation procedures must all be coordinated.
Pharma United Co., Ltd. combines panel manufacturing with cleanroom design, engineering, BIM coordination, equipment supply, and on-site installation. Its manufacturing resources, international experience, factory expansion, and engineering team provide a foundation for customized cleanroom projects in different regions.
Before ordering, clients should confirm the exact core material, surface finish, panel thickness, technical performance, and installation scope. Particular attention should be given to the difference between the named paper honeycomb construction and the rockwool infill listed in the supplied parameter table. Once the configuration is confirmed, the panel can be incorporated into a coordinated cleanroom design that supports efficient construction, reliable operation, and long-term maintenance.
References
1. Cleanroom Design and Construction Principles, technical guidance for controlled-environment facilities.
2. Good Manufacturing Practice principles for pharmaceutical production facilities.
3. General guidance on cleanroom classification, environmental control, and contamination management.
4. Technical literature on honeycomb sandwich panels and cellular-core composite construction.
5. Technical literature on stainless-steel, coated-steel, and high-pressure-laminate surfaces for hygienic interiors.
6. Project-specific product data, manufacturing information, and company profile supplied for Pharma United Co., Ltd.
7. General engineering practice for cleanroom wall, ceiling, door, window, HVAC, and service coordination.
Product: Paper Honeycomb Cleanroom Panel


-
Mobile
+86-177 1554 8238
-
E-mail
chin@pharma-united.com
-
Address
No.58 Beiyuan Road, Dianshanhu Town, Kunshan City, Jiangsu Province, China
Copyright © Pharma United Co., Ltd. Rights Reserved.
OEM/ODM Cleanroom Engineering Solution Manufacturers